Key Points
- Manufacturing quality testing compares materials, processes, and finished products with documented requirements so teams can make defensible acceptance, adjustment, and release decisions.
- Quality assurance designs the system that prevents and detects problems. Quality control applies inspections, tests, and data analysis within that system.
- A result is useful only when the sample, method, measurement system, uncertainty, specification, and decision rule fit the manufacturing question.
- Final inspection can detect some defects. Stable processes, capable measurement systems, and prompt response to variation prevent more of them.
Manufacturing quality testing is the organized examination and measurement of incoming materials, work in progress, and finished products against defined requirements. A quality control laboratory might verify the alloy in a metal part, measure a machined diameter, test a coating’s thickness, examine a weld, or confirm that a packaged device functions as intended.
The laboratory is one part of a larger quality system. Production equipment creates the product, engineering defines what the product must do, suppliers provide materials and components, and quality teams decide how to demonstrate conformity. Testing turns those expectations into evidence. Its value depends on whether the evidence represents the lot or process and whether the measurement can support the decision being made.
What Manufacturing Quality Testing Means
Quality testing asks whether a defined characteristic meets a defined requirement. The characteristic may be dimensional, chemical, mechanical, electrical, optical, functional, or visual. The requirement may come from an engineering drawing, product specification, contract, validated process, regulation, or recognized standard.
The word quality does not mean luxurious or expensive. In manufacturing, it usually concerns consistent fulfillment of stated and implied requirements. A low-cost fastener and a precision implant can both be high-quality products when each reliably meets its intended specifications and use conditions.
A specification states what is required, often with limits or acceptance criteria. A test method describes how the characteristic will be evaluated. A sampling plan determines which units or portions represent a larger lot. A decision rule explains how the result, including relevant uncertainty, will be compared with the requirement. These elements should be settled before data are interpreted.
Quality Assurance, Quality Control, Inspection, and Metrology
Quality Assurance
Quality Control
Inspection
Metrology
These functions overlap without becoming interchangeable. A calibrated micrometer supports a dimensional inspection, while the broader quality system controls who may use it, how often it is checked, what environment is suitable, how results are recorded, and what happens when the instrument is found outside its acceptance limits.
Where Testing Happens in Production
| Stage | Typical Question | Example Evidence | Possible Decision |
|---|---|---|---|
| Supplier qualification | Can the supplier consistently provide the required material or component? | Audit evidence, capability data, certificates, sample testing, and change controls | Approve, conditionally approve, develop, or reject the supplier |
| Incoming inspection | Does the received lot match the purchase specification and identity? | Dimensions, material identity, certificate review, visual condition, or sampled performance | Accept, quarantine, return, or investigate the lot |
| First-piece inspection | Did the setup produce the required characteristics before routine production continues? | Drawing dimensions, surface finish, programmed features, and setup records | Release the setup or correct it before producing the lot |
| In-process control | Is the process remaining stable and centered while production runs? | Control-chart data, sensor readings, operator checks, and periodic samples | Continue, adjust under an authorized rule, pause, or investigate |
| Final inspection or release | Does the product or lot meet the specified release criteria? | Finished-product tests, records review, functional checks, and packaging verification | Release, hold, rework, sort, or reject |
| Post-production monitoring | Are field returns, complaints, or reliability results revealing a recurring problem? | Failure analysis, trend data, retained samples, and service records | Correct the process, change the design, notify affected parties, or monitor |
Testing late in the process can confirm that a product meets requirements, but it may discover problems only after material, machine time, and labor have already been consumed. In-process measurement can reveal drift earlier. Supplier controls can prevent unsuitable material from entering the line. Design reviews can eliminate specifications that are ambiguous or impossible to verify. Effective quality control therefore connects tests across the product life cycle.
Common Manufacturing Test Families
Dimensional and Geometric Measurement
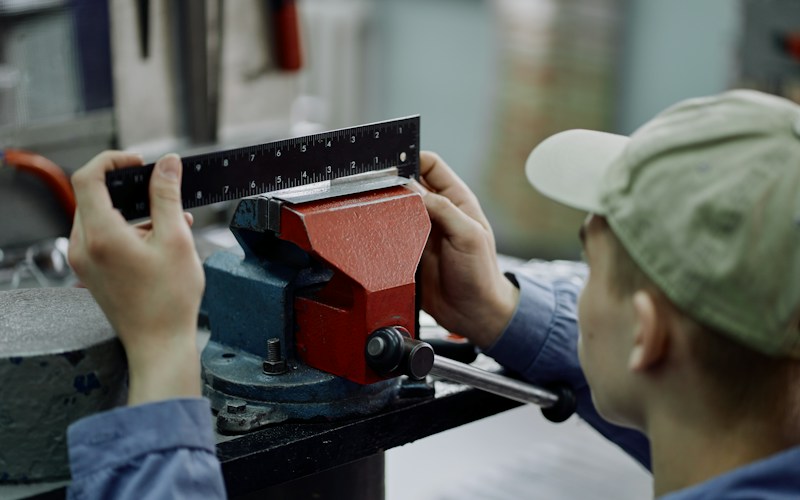
Calipers, micrometers, height gauges, optical comparators, surface-measurement systems, and coordinate measuring machines evaluate size, form, orientation, and location. The drawing, tolerance scheme, fixturing, temperature, surface condition, operator technique, and measurement uncertainty can all influence the result.
Materials and Chemical Analysis
Spectroscopy, chromatography, microscopy, thermal analysis, and elemental techniques can verify composition, contamination, curing, phase, or other material properties. LabPress’s introduction to chemical and materials testing explains how the analytical question, sample preparation, and matrix shape the method.
Mechanical Testing
Tensile, compression, hardness, impact, fatigue, and torque tests examine how a material or assembly responds to force. Some methods consume or permanently alter the test piece, so the sampling plan and specimen preparation must represent the product and manufacturing direction appropriately.
Nondestructive Examination
Visual, ultrasonic, radiographic, magnetic-particle, liquid-penetrant, and eddy-current techniques can reveal selected surface or internal discontinuities without making the examined item unusable. Each technique has limits related to material, geometry, flaw orientation, access, sensitivity, reference standards, and operator qualification.
Functional and Reliability Testing
A functional test challenges the product or subsystem against an operating requirement. Reliability and environmental tests may expose samples to vibration, temperature, humidity, load cycles, or other defined conditions. The protocol must distinguish a production acceptance test from a design-verification or life-testing study.
Visual and Automated Inspection
Human inspectors and machine-vision systems can assess labels, surface condition, assembly presence, color, fill level, or geometry. Lighting, focus, reference samples, defect definitions, viewing distance, software thresholds, and expected variation should be controlled. Automation increases consistency only when the inspection task and decision criteria are well designed.
A Core Quality Testing Workflow
A Concrete Example: A Machined Steel Shaft
Consider a hypothetical steel shaft with a drawing requirement for one outside diameter of 20.000 millimeters, with an allowed variation of plus or minus 0.020 millimeter. The numbers are illustrative and do not represent a universal engineering tolerance.
Before production, engineering and quality staff identify the feature, measurement location, surface condition, unit, tolerance, lot definition, and inspection frequency. They select a suitable micrometer or another dimensional system whose resolution, range, calibration, and uncertainty support the decision. A tool can display more decimal places than the process needs while still being unsuitable because of force, alignment, temperature, surface, or uncertainty.
The inspector checks the instrument’s status and verifies it with the required reference or check standard. A first piece is cleaned, allowed to reach the specified measurement condition, and measured at the defined locations. The inspector records the value and relevant context, including the machine, tool, operator or program identification, and time when the quality plan requires them.
If the first piece conforms and the setup is authorized, production begins. Periodic samples are measured in sequence. A control chart can help the team see whether the process remains stable or whether tool wear, temperature, fixture movement, material variation, or another assignable cause is shifting the results. Control limits are derived from process behavior. The engineering specification limits remain the product requirements. Treating those two kinds of limits as identical would obscure the purpose of each.
Suppose the process data show a sustained upward trend while measured parts are still inside the drawing tolerance. The quality plan may require investigation before a nonconforming part is produced. An authorized response could include checking tool wear, verifying the measurement system, correcting the process, documenting the change, and confirming the result with another sample. Operators should not adjust a stable process in response to every ordinary fluctuation because unnecessary adjustment can increase variation.
If a result falls outside the specification, the affected material is identified and controlled. The team determines the potentially affected production window, verifies the result, evaluates prior measurements, and follows its nonconformance procedure. Rework, sorting, concession, scrap, or another disposition requires the appropriate authority. A single retest should not erase an unfavorable result without a scientifically and procedurally justified investigation.
How to Read Manufacturing Quality Data
Tolerance and Control Limits Serve Different Purposes
Tolerance or specification limits describe acceptable product performance. Control limits describe the expected behavior of a stable process, based on process data and a defined charting method. NIST’s Engineering Statistics Handbook emphasizes this distinction. A process can be stable while producing outside the specification, or unstable while every measured sample still falls inside the specification.
Stability Comes Before Capability
Process capability compares the output of an in-control process with specification limits. A capability index can summarize the relationship, but its interpretation depends on the distribution, sampling, time period, measurement system, and stability assumptions. A favorable index cannot compensate for poor data, an unstable process, or an unsuitable measurement system.
Accuracy and Precision Describe Different Properties
Accuracy concerns agreement with an accepted reference or true value as defined for the measurement. Precision concerns the closeness of repeated measurements under stated conditions. A measurement system may be repeatable and consistently biased, or centered on average with excessive scatter. Calibration, repeated checks, measurement-system studies, and uncertainty evaluation address different parts of this problem.
Traceability Is More Than a Label
NIST defines metrological traceability through a documented, unbroken chain of calibrations or comparisons, with each link contributing to measurement uncertainty. NIST also cautions that traceability alone does not guarantee fitness for purpose. The uncertainty associated with the result must be suitable for the actual measurement need.
Sampling Controls What the Result Represents
A result from one unit directly describes that unit under the test conditions. Extending the conclusion to a lot requires a justified sampling plan and assumptions about lot formation and variation. Random, stratified, periodic, and risk-based approaches answer different questions. Destructive tests create an additional constraint because the tested unit may no longer be saleable.
- Which requirement, revision, and unit of measure govern the decision?
- Does the sample represent the lot, process window, or feature being evaluated?
- Was the method suitable for the material, geometry, range, and tolerance?
- Was the instrument within calibration and controlled under appropriate conditions?
- Were uncertainty and borderline results handled under a documented decision rule?
- Did reference items, blanks, controls, or verification checks perform as expected?
- Is the result connected to the correct item, lot, machine, and record?
- Who has authority to release, reject, rework, or approve a deviation?
Quality Systems and Regulated Manufacturing
ISO 9001:2026 is the current edition of the international quality-management-system standard listed by the International Organization for Standardization. It provides requirements for organizations seeking to demonstrate consistent fulfillment of customer and applicable statutory or regulatory requirements. Certification concerns the management system and its scope. It does not certify that every individual product is defect-free.
Sector requirements can add specific controls. For U.S. medical-device manufacturing, the Food and Drug Administration’s Quality Management System Regulation became effective Feb. 2, 2026. The regulation amended 21 CFR Part 820 and incorporates ISO 13485:2016 by reference while retaining applicable federal requirements and FDA enforcement authority. Manufacturers should consult the regulation, current FDA guidance, and qualified regulatory staff for the products and activities within scope.
A quality control laboratory can support several industries, but methods and records cannot be copied across sectors without assessing intended use. A tensile test for incoming metal, an assay for an active pharmaceutical ingredient, and an electrical safety test for a finished device require different laboratories, competencies, standards, and release structures.
Instrumentation decisions should start with the reportable requirement and complete workflow. LabPress’s guide to choosing analytical instruments by method, matrix, and detection limit provides that framework. Laboratories planning liquid chromatography for regulated quality control can also consult the HPLC and UHPLC systems buyer’s guide. Vendor specifications remain inputs to a method-specific evaluation rather than proof that a system will meet a particular release requirement.
Practical Takeaways for Beginners
Start With the Requirement
Evaluate the Whole Measurement System
Watch the Process
Control Nonconforming Output
New professionals should learn to read drawings and specifications, trace a sample to its lot, check calibration status, distinguish control limits from specifications, and document observations at the time of work. Equipment reliability also matters. LabPress’s preventive maintenance checklist for analytical instruments outlines how laboratories can connect maintenance with method performance, records, and change control.
Frequently Asked Questions
Is quality control the same as quality assurance?
No. Quality control includes operational inspections and tests used to evaluate output. Quality assurance establishes and maintains the larger system that makes those controls reliable, including procedures, training, audits, supplier controls, document management, and corrective action.
Does every manufactured part need to be tested?
The inspection level depends on risk, process capability, customer and regulatory requirements, test destructiveness, economics, and the sampling plan. Some critical characteristics may receive 100% inspection. Other decisions rely on representative samples and process controls.
What is the difference between a specification limit and a control limit?
A specification limit comes from the product requirement and defines acceptable output. A control limit is calculated from process data under a defined statistical method and helps identify unusual process behavior. One should not be substituted for the other.
What does “NIST traceable” mean?
The precise concept is metrological traceability to the International System of Units or another specified reference through a documented chain of calibrations or comparisons, with uncertainty considered at each link. NIST cautions that traceability does not establish that a measurement is fit for every intended use.
Can a passing final test prove the process is under control?
No. A passing test shows that the tested characteristic met its criterion for the examined sample. Process control requires ordered data and evidence that process behavior is stable. The sampling plan determines how broadly the result can be applied.
What happens when a product fails a quality test?
The organization identifies and controls the affected output, verifies the result, assesses scope and risk, investigates as required, and assigns an authorized disposition. Corrective action may address the underlying cause when the problem is systemic or recurring.
Authoritative Sources and Further Reading
- National Institute of Standards and Technology: Policy on Metrological Traceability
- NIST/SEMATECH Engineering Statistics Handbook: Control Charts
- NIST/SEMATECH Engineering Statistics Handbook: Variables Control Charts
- NIST/SEMATECH Engineering Statistics Handbook: Process Capability
- NIST Manufacturing Extension Partnership: ISO and Quality Management
- International Organization for Standardization: ISO 9001:2026
- U.S. Food and Drug Administration: Quality Management System Regulation
Keep Exploring
Related Reading
What Is Pharmaceutical Testing?
A beginner’s guide to pharmaceutical laboratory testing, including specifications, sampling, common analytical tests, batch release, stability work, and scientifically…Read Article
Evaluating Outbreak Testing Methods and Workflow Tradeoffs
A decision framework for public-health outbreak testing, including method comparisons, layered workflows, failure modes, and an actionable laboratory checklist.Read Article
Leave a Reply